

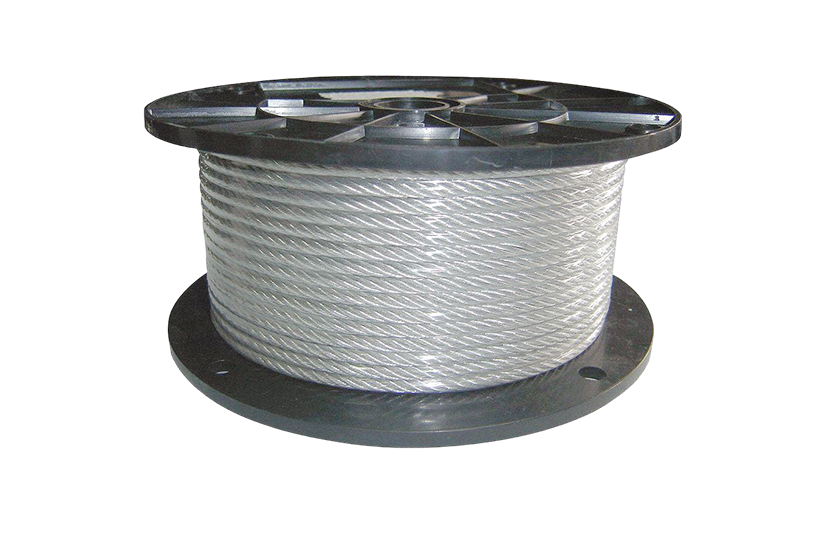
A steel wire rope safety inspection checklist is a structured, practical guide used to evaluate the
condition, performance, and safety of wire ropes in lifting, hoisting, rigging, marine, mining, construction,
material handling, and industrial applications. Because steel wire rope works under high load, bending stress,
abrasion, and environmental exposure, routine inspection is essential to prevent equipment failure, downtime,
injury, and costly operational disruption.
This page provides an SEO-friendly, industry-generic, and fully original overview of steel wire rope
inspection, including definitions, benefits, recommended inspection items, common defects, service criteria,
maintenance guidance, and a clear table format suitable for blogs, directory pages, product support pages, and
industry landing pages. The content is designed for easy insertion into an HTML page and supports ranking-focused
structure with relevant keywords such as steel wire rope inspection checklist,
wire rope safety checklist, wire rope defect inspection, and
steel rope maintenance.
A steel wire rope safety inspection checklist is a formal inspection document or evaluation list used to identify
wear, damage, deformation, corrosion, broken wires, loss of diameter, and other conditions that may reduce the
safe working life of a wire rope. It helps inspectors and operators determine whether a rope is fit for continued
use, requires closer monitoring, or must be removed from service.
In practical use, a checklist standardizes the inspection process so that no critical item is missed. This is
especially important because wire rope damage may not always be obvious from a quick visual glance. A proper
wire rope safety inspection checklist supports preventive maintenance, regulatory compliance, and
safer operation across industries.
Steel wire rope is engineered for strength and flexibility, but it is still a consumable lifting and load-bearing
component. Over time, repeated bending, shock loading, rope speed, contamination, poor lubrication, and harsh
operating environments can weaken the rope structure. Regular steel wire rope inspection helps
detect early signs of deterioration before a failure occurs.
Inspection matters because wire rope failure can lead to:
A well-designed steel wire rope safety inspection checklist provides operational, safety, and cost
advantages. It is not only a compliance tool but also a reliability management tool.
| Benefit | Description |
|---|---|
| Improved Safety | Helps identify dangerous defects before they cause rope failure or accidents. |
| Consistent Inspection | Provides a repeatable method so every rope is checked using the same criteria. |
| Lower Maintenance Cost | Early detection of wear can reduce emergency repairs and unplanned replacement. |
| Longer Rope Life | Proper inspection supports lubrication, correct use, and timely servicing. |
| Regulatory Support | Helps document inspection records for internal compliance and audit readiness. |
| Better Asset Management | Allows planners to forecast replacement timing and inventory needs. |
The inspection checklist below can be adapted to many applications. Steel wire rope is commonly used in:
The following checklist covers the most important visual and functional inspection points. It is suitable as a
general wire rope inspection checklist for industrial use, although specific equipment may require
additional criteria based on manufacturer instructions, local standards, and application conditions.
| Inspection Item | What to Check | Possible Risk | Action |
|---|---|---|---|
| Broken Wires | Count broken wires in any lay length and inspect for clusters or concentrated breaks. | Reduced strength, sudden failure risk | Monitor closely or remove from service depending on severity |
| Abrasion / Wear | Look for flattened outer wires, polished areas, or visible diameter loss. | Loss of load capacity and fatigue resistance | Increase inspection frequency or replace if excessive |
| Corrosion | Check for rust, pitting, moisture damage, and internal contamination indicators. | Weakening of wire strands and internal deterioration | Clean, lubricate, and assess for replacement |
| Diameter Reduction | Measure rope diameter in multiple points and compare with original specification. | Structural deterioration | Replace if reduction exceeds allowable limits |
| Deformation | Inspect for kinks, crushing, birdcaging, waviness, or strand displacement. | Permanent damage and unpredictable performance | Remove from service immediately if severe |
| Lubrication Condition | Check whether the rope is dry, contaminated, or improperly lubricated. | Increased friction, wear, and corrosion | Clean and re-lubricate using approved product |
| End Terminations | Inspect sockets, clips, swages, splices, and fittings for looseness or damage. | Termination failure and load drop | Repair or replace as needed |
| Drum and Sheave Contact | Review rope tracking, drum winding, groove wear, and fleet angle alignment. | Accelerated wear and rope distortion | Correct alignment issues and inspect related components |
| Heat Damage | Look for discoloration, brittleness, welding spatter, or burn marks. | Loss of metallurgical integrity | Remove from service immediately |
| Shock Loading Signs | Check for stretched areas, twisted strands, or sudden distortion after overload events. | Hidden structural damage | Stop use and perform detailed inspection |
Use the following step-by-step checklist during routine visual inspections. This format is suitable for safety
teams, maintenance crews, field operators, and asset management documentation.
| Checklist Step | Inspection Question | Pass / Fail Indicator |
|---|---|---|
| 1. Identification | Is the wire rope type, diameter, construction, and application clearly identified? | Pass if records are available and rope matches application requirements |
| 2. Visual Condition | Is the full visible rope length free from obvious damage, corrosion, and contamination? | Pass if no major visible defects are present |
| 3. Broken Wires | Are there broken wires, especially in high-bend areas near end terminations, drums, or sheaves? | Fail if broken wires exceed acceptable limits |
| 4. Rope Diameter | Has the rope diameter remained within acceptable tolerance? | Fail if measurable reduction is excessive |
| 5. Surface Wear | Are there signs of flattening, abrasion, or outer wire loss? | Fail if wear is severe or accelerating |
| 6. Corrosion Condition | Is rust present only superficially, or is there visible pitting and deep corrosion? | Fail if corrosion is structural or widespread |
| 7. Rope Shape | Is the rope straight, flexible, and evenly wound without birdcaging or kinks? | Fail if deformation is permanent or severe |
| 8. Lubrication | Is lubrication sufficient to protect against friction and moisture? | Pass if rope remains protected and not dry |
| 9. Termination Security | Are clamps, sockets, and fittings secure with no movement or slippage? | Fail if any end fitting is loose or damaged |
| 10. Operating Environment | Has the rope been exposed to chemicals, extreme heat, saltwater, or abrasive dust? | Fail if exposure may have caused hidden damage |
A major part of any steel wire rope safety inspection checklist is recognizing visible and hidden
defects. The table below summarizes common conditions and what they may indicate.
| Defect | Description | Typical Cause | Severity |
|---|---|---|---|
| Broken Wires | Individual outer wires fracture during use. | Fatigue, overload, poor sheave alignment, wear | Medium to High |
| Kink | Permanent sharp bend in the rope caused by mishandling. | Improper installation or shock loading | High |
| Birdcaging | Strands loosen and expand outward from the rope core. | Twisting, sudden load release, torque imbalance | High |
| Crushing | Rope becomes flattened due to compression. | Poor drum spooling or external pressure | High |
| Corrosion | Rust or pitting appears on wires and strands. | Moisture, salt exposure, inadequate lubrication | Medium to High |
| Diameter Loss | Rope becomes thinner than original specification. | Wear, internal deterioration, core damage | High |
| Heat Damage | Rope shows discoloration, hardening, or burn marks. | Welding, fire, friction heat, sparks | High |
| Core Exposure | Internal core becomes visible due to outer layer damage. | Advanced wear or severe deformation | High |
Inspection frequency depends on the rope duty cycle, load severity, environmental exposure, and regulatory or
site-specific requirements. In high-risk applications, inspection may be needed before every shift, daily, weekly,
monthly, and during planned maintenance shutdowns.
| Inspection Frequency | Typical Use Case | Purpose |
|---|---|---|
| Before Use / Pre-Shift | Daily lifting, hoisting, or rigging operations | Detect obvious visible damage before operation |
| Daily | High-use industrial machinery and cranes | Track rapid wear and prevent unsafe operation |
| Weekly | Moderate-duty equipment | Review condition trends and lubrication status |
| Monthly | Lower-duty systems with stable load patterns | Confirm rope health and document maintenance needs |
| Periodic Detailed Inspection | Scheduled maintenance or compliance review | Perform measurement-based assessment and recordkeeping |
A steel wire rope should be removed from service when damage reaches a level that may reduce safe performance. The
exact removal criteria vary by equipment type and governing standard, but common reasons for replacement include:
As a best practice, any rope with sudden damage, unknown history, or questionable integrity should be evaluated by
a qualified person before being returned to service.
A visual wire rope inspection checklist should be performed in a systematic way. Start at one end
of the rope and move along the full accessible length, paying special attention to zones that experience frequent
bending or contact stress.
Good inspection records improve trend analysis and support safer replacement planning. A detailed
steel wire rope safety inspection checklist should include measurable and traceable data.
| Record Item | Why It Matters |
|---|---|
| Date and time of inspection | Creates a traceable maintenance history. |
| Inspector name or ID | Supports accountability and review. |
| Equipment identification | Links rope condition to the correct machine or system. |
| Rope specification | Includes diameter, construction, and duty classification. |
| Inspection findings | Documents defects, wear, corrosion, and unusual conditions. |
| Measured diameter | Helps identify wear trends and replacement thresholds. |
| Action taken | Records whether the rope was cleaned, lubricated, monitored, or replaced. |
| Next inspection due date | Ensures ongoing safety management and scheduling control. |
The following table provides a general reference for common steel wire rope characteristics. Actual specifications
vary by manufacturer, construction type, and intended use.
| Specification Category | Common Options | Typical Use Notes |
|---|---|---|
| Construction | 6x19, 6x36, 8x19, 19x7, compacted strand designs | Different constructions balance flexibility, abrasion resistance, and fatigue life. |
| Core Type | Fiber core, independent wire rope core (IWRC), steel core | Core selection affects strength, crush resistance, and flexibility. |
| Finish | Bright, galvanized, stainless steel | Finish affects corrosion resistance and environment suitability. |
| Lay Direction | Right regular lay, left regular lay, right lang lay, left lang lay | Lay direction affects rotation resistance and handling characteristics. |
| Diameter Range | Small diameter to large industrial sizes | Selected based on load demand, drum size, and system design. |
| Lubrication | Standard factory lubrication, field-applied lubrication | Lubrication helps reduce internal friction and corrosion. |
| Strength Class | Various tensile grades depending on application | Must match equipment and working load requirements. |
Preventive maintenance and inspection go hand in hand. The following practices help extend service life and improve
safety performance:
For content planning and search visibility, the following keyword themes are highly relevant to this topic:
How often should a steel wire rope be inspected?
Inspection frequency depends on duty level, environmental exposure, and local safety requirements. Heavy-use ropes
may require pre-shift inspection, while less demanding applications may follow a weekly or monthly schedule.
What is the most common wire rope defect?
Broken wires, abrasion, corrosion, and diameter loss are among the most common inspection findings. These defects
often indicate fatigue, wear, or environmental damage.
Can a damaged wire rope be repaired?
In many cases, wire rope damage cannot be repaired safely and the rope must be replaced. Severe kinks, birdcaging,
crushing, heat damage, or structural distortion usually require removal from service.
Why is lubrication important?
Lubrication reduces internal friction, helps protect against corrosion, and can extend the service life of the rope
when applied correctly and regularly.
A steel wire rope safety inspection checklist is an essential tool for safe and efficient
operations in lifting, rigging, and industrial applications. By checking for broken wires, wear, corrosion,
deformation, diameter loss, termination condition, and lubrication quality, operators can identify hazards early
and reduce the risk of unexpected failure.
For best results, use a consistent inspection method, document every finding, follow equipment-specific guidelines,
and replace ropes that show signs of serious damage or structural weakness. A disciplined wire rope safety
inspection program protects people, equipment, and productivity while supporting long-term asset
reliability.
```

 Landline Phone: +86-513-85100011
Telephone: +86 13585223056
 E-mail: hangtong@nthangtong.com
vicky@nthangtong.com
 Address: No. 508, Guangxing Road, Baishan Town, Bo'ai County, Jiaozuo City, Henan Province
Copyright © Henan Suxiang Steel Cable Co., Ltd
This website uses cookies to ensure you get the best experience on our website.
 Español
 한국어
 العربية
 Tiếng Việt
 Filipino



 Phone
Comment
(0)