

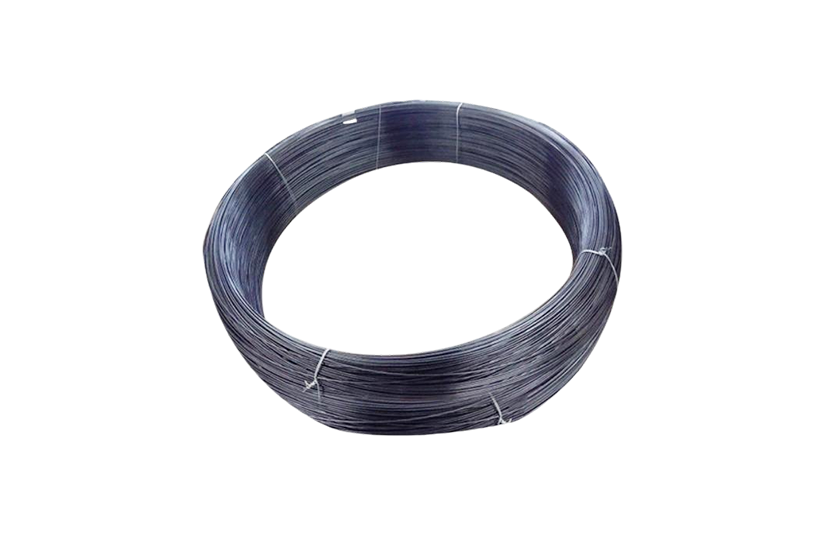
Steel wire rope safety management is a critical part of industrial operations where lifting, pulling, hoisting, tensioning, securing, and load handling are performed on a regular basis. In factories, construction sites, ports, mines, warehouses, offshore platforms, energy facilities, and heavy equipment environments, steel wire rope is often the backbone of safe mechanical operation. Because wire rope works under high stress, repeated flexing, abrasion, vibration, bending, shock loading, and exposure to environmental elements, a structured safety management approach is essential for preventing failure, reducing downtime, and protecting workers and assets.
This guide provides industry-wide information on steel wire rope safety management for industrial operations. It covers the definition of steel wire rope, core advantages, common types, construction basics, inspection methods, safety practices, storage guidelines, selection factors, maintenance routines, and specification tables. The content is written in a search-engine-friendly format and is designed for use in blog posts, category pages, industry pages, resource hubs, and HTML page body sections. It is intentionally generic and does not include specific company recommendations.
Steel wire rope is a mechanical load-bearing assembly made from multiple steel wires twisted into strands, which are then laid around a central core to form a flexible yet strong rope structure. It is engineered to handle tension, lifting, bending, and dynamic loads in industrial environments. Unlike simple cable or chain products, steel wire rope offers a combination of strength, flexibility, and fatigue resistance that makes it suitable for many demanding applications.
Steel wire rope is widely used in overhead lifting systems, cranes, hoists, winches, elevators, rigging setups, dredging operations, offshore lifting, mining equipment, and material handling systems. Safety management for steel wire rope focuses on proper selection, correct installation, routine inspection, controlled use, preventive maintenance, and timely retirement from service.
Steel wire rope failure can lead to dropped loads, equipment damage, production interruption, severe injuries, or fatal accidents. In industrial operations, the consequences of improper rope selection or poor maintenance can be especially serious because wire rope often carries critical loads. A safety management system helps reduce these risks by creating repeatable practices for rope use, inspection, replacement, and recordkeeping.
Key reasons steel wire rope safety management matters include:
Steel wire rope remains one of the most widely used load-handling solutions in heavy industry because of its practical performance characteristics. Understanding these advantages helps businesses choose the correct rope type and apply better safety management practices.
| Advantage | Description | Industrial Value |
|---|---|---|
| High tensile strength | Designed to carry substantial loads under tension | Supports lifting, hoisting, and pulling operations safely |
| Flexibility | Bends around drums, sheaves, and pulleys | Suitable for dynamic mechanical systems |
| Fatigue resistance | Performs well under repeated bending cycles | Useful in cranes, winches, and elevators |
| Durability | Resists wear when maintained correctly | Improves service life in industrial environments |
| Load visibility | Wear and damage can often be inspected visually | Supports routine inspection and early intervention |
| Versatility | Available in many diameters, constructions, and coatings | Can be matched to different applications and conditions |
Steel wire rope is available in several constructions, each with different performance characteristics. Construction influences flexibility, abrasion resistance, fatigue life, and suitability for specific industrial operations. Choosing the right construction is an important part of steel wire rope safety management.
| Construction Type | Typical Characteristics | Common Use Case |
|---|---|---|
| 6x19 | Good abrasion resistance, moderate flexibility | General lifting, winching, industrial hoisting |
| 6x36 | Higher flexibility than 6x19, good fatigue performance | Cranes, mobile lifting equipment, repeated bending applications |
| 8x19 | Balanced flexibility and strength | Elevator systems, hoisting equipment, precision lifting |
| 19x7 | Rotation-resistant construction, strong under load | Crane hoisting lines, non-rotating lifting applications |
| Compact strand rope | Higher metal density, improved strength-to-diameter ratio | Heavy-duty cranes, high-performance lifting systems |
To manage steel wire rope safety effectively, it is important to understand the main components of the rope. Each part affects rope performance and inspection requirements.
Steel wire rope safety management must address the main hazards associated with industrial use. These risks are often related to overloading, poor installation, inadequate inspection, and harsh environmental conditions.
| Risk | Cause | Possible Consequence |
|---|---|---|
| Overload | Load exceeds the rope’s safe working limit | Rope breakage, dropped load, equipment damage |
| Fatigue failure | Repeated bending over sheaves or drums | Progressive wire breakage and reduced rope life |
| Abrasion | Rope rubs against metal surfaces or rough structures | Outer wire wear and reduced load capacity |
| Corrosion | Exposure to moisture, chemicals, salt, or humidity | Internal and external weakening of wires and strands |
| Kinking or twisting | Improper handling or installation | Permanent distortion and reduced strength |
| Shock loading | Sudden application of force | Unexpected stress spikes and accelerated wear |
| Poor lubrication | Insufficient maintenance or wrong product use | Internal friction, heat buildup, and corrosion |
Routine inspection is one of the most important parts of steel wire rope safety management. Inspections should be performed before use, during scheduled maintenance, and after any abnormal event such as overload, impact, or excessive wear. Visual inspection alone is helpful, but for critical operations it should be combined with documented maintenance and periodic evaluation.
| Inspection Item | What to Check | Why It Matters |
|---|---|---|
| Broken wires | Count visible wire breaks along the length and at contact points | Signals fatigue and possible end-of-life condition |
| Corrosion | Look for rust, pitting, discoloration, or moisture damage | Indicates internal weakening and reduced durability |
| Wear | Check for thinning, flat spots, and polished areas | Shows loss of metal and reduced load capability |
| Deformation | Inspect for kinks, crushing, birdcaging, or strand separation | Can indicate structural damage and unsafe service conditions |
| Lubrication condition | Verify whether the rope is properly lubricated and clean | Supports fatigue resistance and corrosion protection |
| End fittings | Examine clips, sockets, thimbles, and terminations | Termination failure can cause total system failure |
| Drum and sheave condition | Check grooves, alignment, wear, and surface condition | Improper contact can accelerate rope damage |
Replacement criteria should be defined in site safety procedures and should follow applicable operational standards. Even when wire rope still appears functional, hidden internal damage may make it unsuitable for continued service. Timely replacement is safer and often more economical than continuing to operate damaged rope.
Common replacement triggers include:
For safety-critical industrial operations, a rope should be removed from service immediately when damage is identified that could affect safe operation. Inspection records should be maintained to support replacement decisions.
Proper selection is central to steel wire rope safety management. The right rope must match the load requirements, operating environment, bending frequency, equipment design, and maintenance capability. A rope selected only by diameter or price may not perform safely in real industrial use.
| Selection Factor | Consideration | Typical Impact |
|---|---|---|
| Working load | Expected maximum load and safety factor | Determines minimum strength requirement |
| Flexibility need | How often the rope bends over sheaves or drums | Affects strand construction choice |
| Abrasion exposure | Contact with rough surfaces or frequent rubbing | May require more abrasion-resistant construction |
| Corrosion exposure | Outdoor, marine, chemical, or wet environments | May require coating, lubrication, or special core |
| Rotation resistance | Need to control rope spin under load | Important for crane and lifting systems |
| End termination | Compatibility with sockets, clips, or swages | Must match the installation design |
| Operating temperature | Heat or cold conditions at the worksite | Can influence lubrication and material performance |
The following table provides a general specification overview for common Industrial Steel Wire rope categories. Exact values vary by manufacturer, construction, wire grade, core type, and standard. This table is intended for general SEO and educational use only.
| Specification | Typical Range / Example | Notes |
|---|---|---|
| Diameter range | 4 mm to 80 mm+ | Industrial applications may use smaller or much larger diameters |
| Construction | 6x19, 6x36, 8x19, 19x7, compacted rope | Construction affects flexibility and wear resistance |
| Core type | Fiber core, independent wire rope core, steel core | Core choice affects strength, support, and heat resistance |
| Surface finish | Bright, galvanized, coated | Finish helps address corrosion and environment exposure |
| Strength grade | Various tensile classes | Higher grades offer higher load capacity |
| Lubrication | Factory-applied or maintenance-applied | Important for internal wear and corrosion control |
| Rotation behavior | Standard or rotation-resistant | Rotation-resistant rope reduces load spin |
| Typical applications | Cranes, hoists, elevators, winches, mining, rigging | Selection should match specific operating conditions |
Handling practices directly affect rope life and safety. Even a high-quality rope can fail early if it is twisted, dragged, bent sharply, or installed incorrectly. Industrial teams should train workers to handle rope with care from storage to installation and throughout daily operation.
Proper storage is an essential part of steel wire rope safety management, especially in humid, coastal, outdoor, or chemically aggressive environments. When rope is stored correctly, its lubrication remains effective and corrosion risk is reduced.
| Storage Practice | Recommended Action | Benefit |
|---|---|---|
| Dry environment | Store rope in a clean, dry, covered area | Reduces corrosion risk |
| Elevation | Keep reels off the floor when possible | Prevents moisture contact and contamination |
| Protection | Use coverings or packaging where appropriate | Helps maintain lubrication and finish |
| Rotation of stock | Use older stock first when suitable | Limits long-term degradation in storage |
| Regular checks | Inspect stored rope for rust, damage, or coil distortion | Allows early corrective action |
Preventive maintenance helps extend the service life of steel wire rope and supports safer industrial operations. Maintenance should be planned according to usage intensity, environmental exposure, and equipment type.
Steel wire rope is used across many industrial sectors because it performs reliably under heavy-duty mechanical stress. Safety management practices may differ by sector, but the core principles of inspection, maintenance, and correct selection remain the same.
| Industry | Typical Application | Primary Safety Focus |
|---|---|---|
| Construction | Crane lifting, hoisting, material handling | Load control, inspection, and proper rigging |
| Mining | Hoists, haul systems, tensioning | Abrasion resistance and fatigue management |
| Marine and offshore | Winches, mooring, lifting systems | Corrosion protection and load monitoring |
| Manufacturing | Hoists, conveyors, equipment support | Routine inspection and controlled operation |
| Transportation and logistics | Cranes, loading equipment, securing systems | Safe working load compliance |
| Energy and utilities | Tensioning, lifting, maintenance equipment | Durability and environmental resistance |
A practical steel wire rope safety management program can be built around five core steps: choose correctly, install correctly, inspect regularly, maintain consistently, and replace on time. This framework supports both operational efficiency and workplace safety.
For content planning and on-page SEO, the following keyword phrases are commonly associated with steel wire rope safety management for industrial operations:
| Term | Meaning |
|---|---|
| Safe working load | The maximum load a rope system is intended to carry under normal conditions |
| Breaking strength | The load level at which the rope may fail under test conditions |
| Fatigue | Progressive weakening from repeated stress cycles |
| Birdcaging | A deformation where outer strands open outward due to internal imbalance |
| Kinking | Permanent distortion caused by improper bending or handling |
| Corrosion | Material loss caused by chemical reaction with the environment |
| Termination | The method used to attach rope ends to equipment or fittings |
Steel wire rope safety management for industrial operations is not just a technical requirement; it is a core safety discipline that protects workers, equipment, and productivity. By understanding wire rope construction, advantages, risks, inspection rules, selection factors, storage needs, and replacement criteria, industrial organizations can create safer and more reliable operations. A structured program built around proper handling, preventive maintenance, and timely retirement from service helps extend rope life while reducing the likelihood of failure.
Whether used in lifting, hoisting, mining, construction, offshore work, or heavy manufacturing, steel wire rope must always be managed with care. Consistent safety practices, detailed inspection routines, and well-defined maintenance procedures are the foundation of effective industrial wire rope safety management.
```

 Landline Phone: +86-513-85100011
Telephone: +86 13585223056
 E-mail: hangtong@nthangtong.com
vicky@nthangtong.com
 Address: No. 508, Guangxing Road, Baishan Town, Bo'ai County, Jiaozuo City, Henan Province
Copyright © Henan Suxiang Steel Cable Co., Ltd
This website uses cookies to ensure you get the best experience on our website.
 Español
 한국어
 العربية
 Tiếng Việt
 Filipino



 Phone
Comment
(0)